Engineered for extreme structural durability, high refresh rates, and seamless interactive visual environments.
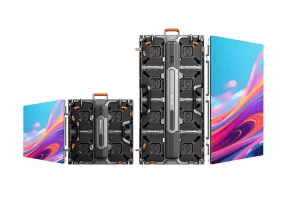
How advanced load-bearing design, GOB surface sealing, and optical glass masks enable high-footfall interactive ground environments.
Reinforced aluminum alloy chassis and high-tensile steel sub-structures deliver a certified static load capacity exceeding 2,000 kg/m². Perfect for automotive launch events, heavy machinery expos, and high-density pedestrian zones.
Glue-on-Board (GOB) technology encapsulates SMD LEDs under a crystal-clear epoxy resin shield. Provides IP65/IP67 waterproof protection, impact resilience, scratch resistance, and easy cleaning against liquid spills.
Custom high-transmittance polycarbonate masks with micro-frosted anti-glare coatings diffuse direct light, preventing moiré patterns on broadcast cameras while preserving wide 160° viewing angles.
Industrial ground LED displays require fundamental deviations from standard vertical video wall design. When selecting a wholesale LED floor display factory, global procurement teams must audit the structural frame's modulus of elasticity and dynamic stress resistance. Modern high-tier interactive floor panels utilize die-cast aluminum sub-frame columns with dual-layer shock absorption pads. This structure prevents micro-flexing of the printed circuit board (PCB) when subjected to sudden impact loads, such as dancers landing or vehicle wheels rolling across panel seams.
Furthermore, thermal dissipation within enclosed ground channels presents unique operational challenges. Unlike vertical screens that leverage natural upward convection, floor displays trap thermal energy under non-conductive floor tiles. Advanced manufacturing integrates heat pipes linked directly to aluminum heat-sink bases, maintaining LED junction temperatures below 65°C even during continuous 24/7 operation at peak luminance (up to 4,500 nits for outdoor environments).
| Performance Parameter | Indoor Interactive Floor LED | Outdoor Heavy-Duty Floor LED | XR Virtual Stage Floor LED |
|---|---|---|---|
| Pixel Pitch Range | P1.95 - P3.91 mm | P3.91 - P6.25 mm | P1.56 - P2.60 mm |
| Load Bearing Capacity | 1,500 - 2,000 kg/m² | 2,000 - 3,500 kg/m² | 2,000 kg/m² (Rigid Structure) |
| Ingress Protection (Front/Rear) | IP54 / IP43 (GOB Protected) | IP65 / IP67 Fully Sealed | IP54 (Anti-Reflective Mask) |
| Refresh Rate & Scan | 3,840 Hz (1/16 Scan) | 3,840 Hz - 7,680 Hz | 7,680 Hz (Low Latency <1 frame) |
| Sensor Technology | Optoelectronic Pressure Matrix | Radar / Infrared Framing | Camera Motion Tracking Sync |
Transform static ground surfaces into responsive digital canvases using embedded optical micro-sensors and AI rendering engines.
Unlike external camera-tracking systems that suffer from line-of-sight occlusion, our factory integrates infrared optical sensor chips directly onto the PCB substrate. Every cabinet features up to 16 point-sensors that detect pressure and footstep proximity instantaneously, enabling precise fluid particle interactions and dynamic visual response.
Fully compatible with NovaStar, Colorlight, and Unreal Engine interactive software pipelines. The floor system feeds raw sensor coordinates via Gigabit Ethernet directly to interactive graphics servers, rendering 60 FPS 3D physics simulations—such as breaking ice, expanding ripples, or digital path tracking—underfoot in real-time.
Unlocking commercial value across diverse physical architecture and high-traffic public installations.
Car manufacturers utilize high load-bearing LED floor display tiles to create virtual driveways. Vehicles park directly on top of the display wall, showing dynamic energy flow visuals beneath the tires during launch keynotes.
Modern film studios combine LED floor tiles with curved vertical background walls. Matched pixel pitch and 7,680Hz refresh rates eliminate moiré effect, letting camera operators capture realistic parallax perspectives.
High-end flagship stores integrate interactive floor panels in main entry foyers. Footsteps generate interactive branded elements, boosting dwell time by over 45% and encouraging social media user-generated content.
Immersive historical exhibits recreate ancient riverbeds or cosmic space environments on ground screens. Visitors physically walk through animated historical timelines with instant tactile visual feedback.
Smart LED basketball courts feature programmable lines, instant replay underfoot, dynamic player tracking, and sponsor branding transitions during timeouts—replacing static wooden flooring.
IP65 outdoor floor displays transform municipal public squares into night-time tourism hot spots. Anti-wear coatings withstand heavy street traffic, extreme weather, and continuous public exposure.
Why leading global distributors source directly from Shenzhen’s automated manufacturing clusters.
Shenzhen, China represents the epicenter of global optoelectronic manufacturing, controlling over 90% of the worldwide LED screen production ecosystem. Sourcing from a specialized wholesale LED floor display factory offers unmatched cost efficiencies, technical precision, and rapid scalability. Our production center utilizes high-speed Yamaki and Panasonic SMT placement lines capable of mounting micro-scale SMD LED chips with ±0.01mm placement accuracy.
Quality assurance protocols for ground LED screens require far more rigorous testing than traditional vertical displays. Every module produced undergoes a stringent multi-stage inspection sequence:
Modules undergo thermal cycling from -40°C to +80°C alongside high-frequency mechanical vibration simulation to verify solder joint integrity before encapsulation.
Randomized sample cabinets are subjected to 2,500 kg hydraulic point-presses for 24 continuous hours to confirm zero deflection in structural support pillars.
Every assembled panel is operated at 100% peak brightness for 72 continuous hours in aging chambers to identify and eliminate early-stage component failure.
Anticipating hardware breakthroughs: Micro-LED, AI-predictive interaction, and zero-carbon driver IC architectures.
The next technological leap will transition ground panels from traditional SMD/GOB to Micro-LED technology. Sub-P1.2 pitch floor screens will enable ultra-high pixel density ground displays, allowing visitors to stand inches away from ultra-HD visuals without seeing pixel grain.
Integrating neural-network processing directly into the screen’s receiving card firmware will allow the display to anticipate human walking direction, rendering fluid dynamics ahead of the footstep for zero perceived latency.
By precisely powering Red, Green, and Blue LEDs at their exact forward voltage requirements, common-cathode driver architectures reduce power consumption and heat generation by up to 40%, significantly extending screen lifespan.
Future optical protective covers will incorporate shape-memory polyurethane coatings capable of repairing superficial high-heel and equipment scuffs automatically under ambient sunlight or low heat application.
Meeting stringent global regulatory, safety, and mechanical engineering standards for commercial installations.
Certified to meet CE (EMC & LVD), FCC Class A, RoHS, and ETL standards. All power units utilize PFC (Power Factor Correction) supplies exceeding 95% efficiency, satisfying strict regional grid requirements.
Engineered with high-traction surface textures verified to meet DIN 51130 R11/R12 slip resistance ratings, ensuring public safety even when wet during outdoor rains or liquid spills.
Featuring magnetic suction and top-accessible latch mechanisms. Individual LED modules or power boxes can be extracted from the installed floor in under 30 seconds using specialized vacuum lift tools without dismantling adjacent tiles.
Answers to technical, engineering, and logistic questions from system integrators and AV rental companies.
From COB fine-pitch conference machines to stadium perimeter walls and smart city digital signage.